

Conditioning chemicals
When Veolia Environmental CHOCOLATE MOULDS
Services required a specialist
conditioning chemical
supplier for the boiler water
at its Tyseley energy recovery
facility it turned to ELGA
Process Water for help. The
plant
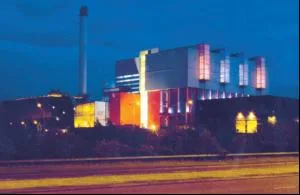
When Veolia Environmental CHOCOLATE MOULDS
Services required a specialist
conditioning chemical
supplier for the boiler water
at its Tyseley energy recovery
facility it turned to ELGA
Process Water for help. The
plant incinerates 350,000t of
Birmingham’s non-recyclable
rubbish each year and
exports 25MW of electricity
to the National Grid, enough
to power 41,000+ homes.
The facility has two 45bar
400°C water tube boilers
delivering 67t/h of steam to
the high pressure turbines. It
also has a 10bar waste heat
shell boiler fuelled by a
clinical waste incinerator, and
this supplies steam to a low
pressure turbine.
To maximise efficiency, the
quality of the water fed to the
boilers has to be carefully
controlled. Tyseley produces
high purity deionised water
on site and adds chemicals to
scavenge oxygen and adjust
the pH to prevent corrosion.
The combination of two
types of boiler with common
feed water and condensate
systems meant that
controlling the boiler water
chemistry at Tyseley required
a specialist solution.
ELGA Process Water, a
Veolia Water Solutions &
Technologies company,
carried out a survey with
technical support from its
boiler competence centre. A
solution was developed
which included chemicals
from its Hydrex range to
provide protection of the
boilers, turbines and
condensate system, as well as
recommendations for regular
service support to maintain
ongoing boiler efficiency and
optimal performance.
IPE Newsletter
IPE publishes a weekly eNewsletter, delivering a carefully chosen selection of the latest stories straight to your inbox.
Subscribe here