

Sauce role for infrared oven
A custom-designed, carbon
infra-red oven from Heraeus
Noblelight is helping
Premier Foods achieve
efficiency gains of more than
10% over a former hot rinse
system on the cooking sauce
production line at its Bury St
Ed
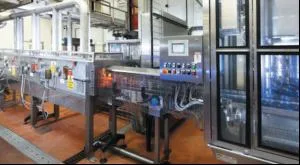
A custom-designed, carbon
infra-red oven from Heraeus
Noblelight is helping
Premier Foods achieve
efficiency gains of more than
10% over a former hot rinse
system on the cooking sauce
production line at its Bury St
Edmunds plant.
After cooking, sauce is
pasteurised in-line and
delivered to the jar filler at
94°C. The new set-up saves
space and time by
eliminating the need for a flat
bed pasteuriser post bottling.
Premier approached
conveyor system manufacturer,
SFT-UK, who recommended
a Heraeus infrared oven for
glass jar heating. Tests proved
the capability of medium
wave infrared in heating glass
jars effectively. A 124kW
infrared oven was installed on
the production line. SFT-UK
modified the line, removing
the hot water jar rinser and
installing a Paxona SFT
sidegrip jar inverter/ filtered
air cleaner.
The oven was installed
immediately after the air
cleaner. Stainless steel, it is in
two sections, one with four
24kW zones and one with
two 13.8kW zones. An
optical pyrometer measures
the temperature of the jars as
they leave the oven; the
temperature is shown on the
front control panel.Manual
or automatic control can be
selected. All infrared emitters
have failure detection so that
the line is shut down in the
unlikely event of emitter
failure. If the line needs to be
stopped for any reason, the
carbon emitters switch off
virtually instantaneously.
The new oven has proved
a success, not only with
production management in
terms of less downtime and a
10% increase in line speed,
but with the workforce too.
IPE Newsletter
IPE publishes a weekly eNewsletter, delivering a carefully chosen selection of the latest stories straight to your inbox.
Subscribe here