

From catastrophic failure to zero tube failures
VPK Packaging’s corrugated plant in Somerset lost its first boiler to caustic embrittlement failure after five years of acceptable monthly test results. The replacement boiler, now six years in, has had zero tube failures on a line running 24/5 with no margin for downtime
AT VPK Packaging’s corrugated packaging plant in Wellington, Somerset, a single horizontal three‑pass fire‑tube boiler supplies steam to a high‑volume corrugator that runs 24 hours a day, five days a week, with additional weekend production during busy periods.
Steam is used to heat preheaters, corrugating rolls, steam showers and starch mixers, so any loss of steam would halt production and undermine VPK Packaging’s ability to serve South Wales, the South West and the South of England from this strategically located hub. "Uptime is everything on a corrugator, so the boiler simply has to keep running," explained Gregory Pow, corrugator engineer at VPK Packaging.
Overcoming boiler failure
Before Deep Water Blue’s involvement, VPK Packaging’s first boiler at its Wellington site suffered repeated tube issues and ultimately catastrophic failure traced to caustic embrittlement. Despite apparently acceptable monthly results from a previous water treatment supplier, daily checks sat with corrugator operators who recorded data inconsistently, masking episodes where pH drifted outside the safe range.
Non‑destructive testing in year five revealed catastrophic failures of the plant including extensive cracking around the burner tube and tube plates, leaving the boiler beyond economic repair and forcing VPK Packaging to rely on a hire boiler for approximately nine months while a permanent replacement was installed.
Turning to a steam specialist
When VPK Packaging invested in the new fire‑tube boiler, the business deliberately sought a specialist in steam boiler water treatment rather than a generalist water company. VPK Packaging put Pow through BOAS training, while also engaging with Deep Water Blue’s water treatment specialists who subsequently visited the Wellington site to assess the boiler house, condensate recovery system and broader compliance landscape.
Pow reports that Deep Water Blue’s deep involvement in UK boiler guidance through the Combustion Engineering Association gave VPK Packaging confidence that the programme would reflect BG01 expectations and UK‑specific legislation rather than generic European standards.
"We focus on steam plant from the ground up, which allows us to design chemistry, testing and digital oversight around each boiler’s risk profile and duty, not around a generic template," said George Nixon, water treatment specialist at Deep Water Blue.
Transforming daily boiler care
Deep Water Blue replaced the old single‑pot amine treatment with a three-component dosing programme to suit the steam boiler and condensate recovery system, and secure reliable sulphite delivery.
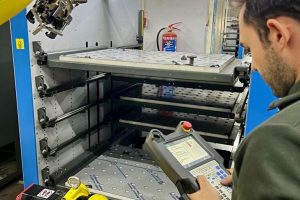
Pow and his team now complete a comprehensive and disciplined daily water treatment testing routine, as well as visual checks, blowdowns and evaporation tests. All results are entered into Deep Water Blue’s vSteam digital management platform, where the VPK team records every test, chemical adjustment and operational note.
"I particularly value the ability to review ten‑day trends at a glance, check that auto‑blowdown aligns with manual TDS readings and spot issues such as falling sulphite well before they threaten asset integrity," he said, adding that during weekend downtime, the team uses weekday data in vSteam to fine‑tune pump settings so the boiler holds protective sulphite levels in unattended periods without wasting chemical.
"We designed vSteam to make detailed boiler testing feel manageable, giving engineers instant visibility of trends and the context behind every reading so that small deviations never snowball into big failures," Nixon continued.
Taming a highly efficient condensate system
VPK Packaging’s condensate recovery system introduced both an opportunity and a challenge. Large volumes of clean condensate return to the boiler thanks to the installed Baviera system, significantly reducing make‑up water demand to roughly 20 cubic metres per week on a seven‑day firing schedule, but also diluting oxygen scavenger and other conditioning chemicals. Working closely with Deep Water Blue, VPK Packaging installed an additional dosage point for the oxygen scavenger tied to the condensate recovery system’s pump speed, so dosing automatically tracks condensate flow and maintains protection even as production rates change.
This collaborative troubleshooting contrasts sharply with Pow's experience of previous providers, where apparently acceptable snapshot readings masked underlying instability. He believes that the three-way partnership with Deep Water Blue, the condensate recovery system manufacturer, and the steam boiler OEM has given VPK Packaging fresh insight into condensate systems at other sites with similar configurations.
Improvements in reliability, leaks and chemical use
Since adopting Deep Water Blue’s programme and vSteam platform, VPK Packaging’s Wellington facility has experienced a striking shift in reliability. In the six years since the replacement boiler was installed, the only significant issue has been a manufacturing‑related weld defect on the feedwater inlet, unrelated to water treatment and resolved by rewelding a tube. Pow reports no tube failures at all on the current boiler, describing the difference compared with the original unit as "night and day".
The benefits reach far beyond the boiler shell. Historically, VPK Packaging’s Wellington site wrestled with frequent gasket failures and steam leaks around preheaters, often repairing a leak every four to six weeks. "Since partnering with Deep Water Blue, those leaks have almost disappeared," Pow stated, noting that he struggles to recall the last time he had to tackle a steam leak and estimating intervals of three to four months or more between incidents.
Chemical consumption has also stabilised at what Pow considers a modest level, with Deep Water Blue adjusting sulphite set‑points to provide a buffer over unattended weekends while keeping pump outputs low.
Deep Water Blue aims to tune each boiler so that protection is robust without being wasteful, which is why they see sites like VPK Packaging’s Wellington facility ordering chemical less frequently even as they increase the depth and frequency of their testing, Nixon stated.
Changing attitudes to water treatment
The combination of BOAS‑trained on‑site personnel, Deep Water Blue’s water treatment specialists and the vSteam audit trail has transformed how VPK Packaging views boiler compliance and risk.
"Many industrial sites still underestimate water treatment, only discovering its importance when everything has stopped, it is all going wrong and regulators arrive to investigate. My experience of a five-year-old boiler failing through caustic embrittlement has made me acutely aware that cutting corners on treatment or switching to cheaper suppliers can carry a far higher long‑term cost," said Pow.
"Once you develop the trust that we have with Deep Water Blue, it is very hard to trust anyone else." In particular, he highlighted the extensive phone support, shared documentation and joint problem‑solving with Deep Water Blue’s team, especially during the early years with the new boiler.
"Given variations in local water quality, plant design and duty, water treatment and boiler care must remain site specific rather than being standardised across sites or even countries," he emphasised.
For more information:
Tel: +44 870 460 2980
Related posts
IPE Newsletter
IPE publishes a weekly eNewsletter, delivering a carefully chosen selection of the latest stories straight to your inbox.
Subscribe here