Why refrigerant and compressor design decide the long-term efficiency of industrial heat pumps
INDUSTRIAL HEAT pump adoption remains low, well below the roughly 20% percent of industrial heat demand the IEA says commercially available systems could technically already supply, despite offering three to four times the efficiency of a conventional gas or oil boiler.
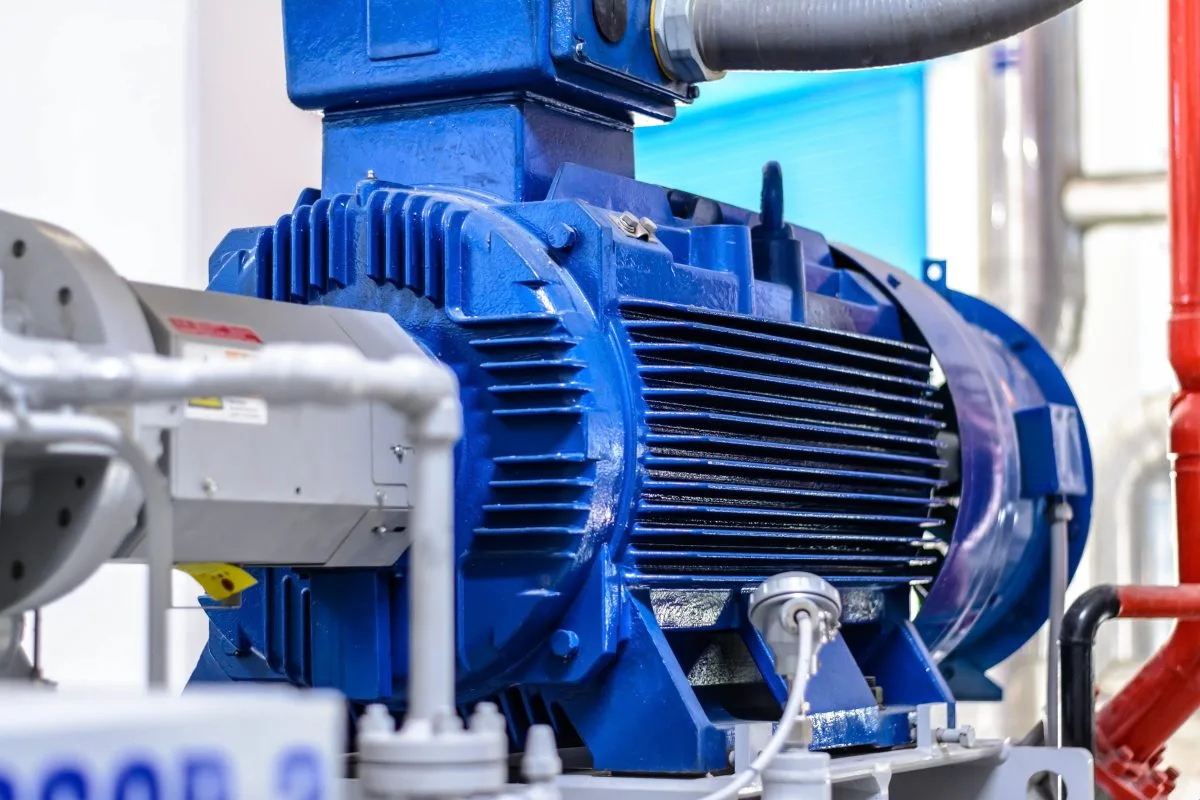
That gap between technical merit and market uptake is closing, but slowly. Most specification conversations centre on temperature lift, capacity and payback period.
Two decisions that shape what happens to that efficiency over the following decade get far less attention: which refrigerant sits inside the machine, and how the compressor manages lubrication.
The industrial heat pump market has a blind spot on refrigerant and compressor selection
Industrial heat pumps, defined as units above 200 kilowatts thermal, are on course to grow more than 15% percent per year to 2030 as industry and district heating networks push to decarbonise. Refrigerant choice and compressor architecture usually appear as separate line items on a spec sheet, one treated as an environmental compliance question and the other as a mechanical reliability question, so assessed on their own, both look manageable on paper.
Assessed together, they determine how much of a heat pump’s rated efficiency survives ten years of continuous operation, and that link rarely makes it into a specification document.
Refrigerant class sets the safety envelope a compressor has to be built around. Compressor lubrication design determines whether the refrigerant side of the system keeps delivering the coefficient of performance (COP) printed on the datasheet. A strong choice on one axis can’t fully offset a weak choice on the other.
How F-Gas regulation is narrowing refrigerant options for large-scale systems
Large heat pumps and chillers above 12 kilowatts face a genuine market restriction from January 2027: only refrigerants with a global warming potential (GWP) below 750 will be permitted on new equipment, under the revised EU F-Gas Regulation (2024/573). For a specifying engineer, this date matters at the point of order. A system ordered on a higher-GWP refrigerant still has to clear manufacturing and installation lead times, and if those run past January 2027, the refrigerant decision made today determines whether the finished system can be placed on the market at all.
Many HFC refrigerants still installed in industrial systems today sit well above that limit.
Specifying a system now on one of these refrigerants means either a shortened service life ahead of a forced retrofit, or a refrigerant transition cost that never appears in the original quote. At industrial scale, that’s a capital planning problem, and it needs pricing into the original proposal in order to avoid an unbudgeted retrofit years into operation.
The regulation restricts what can be newly placed on the market from 2027. It doesn’t remove existing equipment from service on the same date in most cases. That’s why refrigerant selection now needs sign-off from procurement as well as engineering: get it wrong at the ordering stage, and a system can be non-compliant before it’s even commissioned.
Natural refrigerants at industrial scale: ammonia, CO2 and hydrocarbons compared
No single natural refrigerant suits every industrial application. Ammonia (R717) carries zero ozone depletion potential and zero GWP, and it delivers strong thermodynamic performance at the pressures and temperatures typical of large heat pump duty. It’s toxic and mildly corrosive to copper alloys, which rules out standard copper pipework in favour of steel, and it calls for trained personnel and containment measures consistent with COSHH and a site-specific risk assessment.
Carbon dioxide (R744) runs a transcritical cycle at working pressures well above ammonia or hydrocarbon systems, often above 100 bar on the high side. That pressure profile suits applications needing a large temperature lift or a high discharge temperature, at the cost of heavier-duty components throughout the circuit.
Hydrocarbons, principally propane (R290), sit at the low end of the GWP scale among natural refrigerants: 0.02 under the IPCC’s sixth assessment methodology, referenced in Annex VI of EU Regulation 2024/573, against a figure of 3 still quoted in older technical literature based on the fourth assessment report. R290 carries an A3 classification under ASHRAE Standard 34: low toxicity, high flammability. That classification shapes the engineering brief around the compressor and electrical system.
What flammability class means for compressor design
An A3 rating under ASHRAE 34 governs the safety envelope built around a compressor.
Electrical equipment inside the circuit has to meet IEC/EN 60079-15 for spark-free operation, refrigerant charge is capped by application, and the system needs leak detection, ventilation design and terminal protection to a standard a synthetic-refrigerant system doesn’t require.
Screw, reciprocating, scroll and turbo compressors are all manufactured for hydrocarbon refrigerants, so flammability class is a safety and electrical design driver more than a mechanical architecture constraint.
That added engineering scope is what makes a propane-based system and an HFC-based system of similar capacity rarely land at the same installed cost. It belongs in a total-cost-of-ownership comparison.
Why compressor lubrication design is the overlooked efficiency variable
Oil-lubricated compressors, whether screw, scroll or reciprocating, carry a small but persistent quantity of lubricating oil into the refrigerant circuit during normal operation. Over time, that oil deposits as a thin film across evaporator and condenser surfaces. That film acts as an insulating layer on the heat exchanger, and it pulls heat transfer efficiency below the value the compressor was originally rated against.
This is expected behaviour for oil-lubricated technology, which is exactly why these systems are specified with maintenance intervals for oil analysis, filter changes and periodic oil recovery. The efficiency loss builds gradually. That makes it easy to miss at specification stage and expensive to trace once COP has drifted below the commissioning figure years into operation.
Oil-free turbocompressors remove that mechanism from the system. These are gas-bearing designs: the rotating shaft rides on a thin film of compressed gas rather than a mechanical bearing lubricated by oil, so no lubricant ever enters the refrigerant circuit. Heat exchanger surfaces stay clean for the working life of the machine, and COP holds closer to its commissioned figure instead of drifting against a maintenance clock.
That’s a shift in compressor architecture, and it’s happening in a capacity range long dominated by oil-lubricated scroll and rotary compressors. Oil-free turbocompressor designs are now being built specifically around hydrocarbon refrigerants like R290.
Energy recovery from waste heat: where the two decisions compound
The case for industrial heat pumps has always rested partly on waste heat recovery: pulling low-grade heat from processes, effluent streams or ambient sources and upgrading it to a usable temperature at a fraction of the primary energy cost of combustion. That case strengthens or weakens depending on the discharge temperature the system can sustain, and discharge temperature is exactly where refrigerant choice and compressor lubrication design meet.
Higher discharge temperatures, the kind needed for process reheating, push compressors toward tighter operating tolerances. Oil-lubricated systems run into a real limit here. Mineral and synthetic lubricants have thermal stability ceilings, and operating close to those ceilings shortens oil life and accelerates the heat exchanger fouling described above. A system with no oil in the circuit doesn’t carry that particular constraint, which widens the practical temperature range available for waste heat recovery without the maintenance penalty that comes from pushing an oil-lubricated system toward its thermal limit.
For a facilities engineer evaluating waste heat recovery from a process running at 60 to 90 degrees Celsius, the relevant question is whether it can hold that temperature at full duty cycle for a decade without the efficiency curve bending downward.
A specification checklist for evaluating industrial heat pump refrigerant and compressor combinations
Before shortlisting a heat pump supplier, a specifying engineer should get clear answers to the following:
- What refrigerant is used, and what GWP figure applies under the current IPCC assessment methodology, rather than an older and more flattering one?
- What ASHRAE 34 or ISO 817 flammability and toxicity classification applies, and what does that mean for electrical design, charge limits and site containment?
- Is the compressor oil-lubricated or oil-free? If oil-lubricated, what maintenance interval manages oil carryover and heat exchanger fouling?
- What COP figures are quoted at full and part load, and are they based on an independent test standard such as EN 14511 or on manufacturer in-house testing?
- What discharge temperature can the system sustain at full duty cycle without accelerated wear, and over how many proven run-hours or start cycles has that been demonstrated?
- How does the 2027 GWP threshold for the relevant capacity band affect this system’s market availability across its expected service life?
Most vendor data sheets won’t answer these questions unprompted. Asking them directly is what turns refrigerant and compressor selection from a compliance checkbox into a decision made with the full picture of long-term operating cost in view.
IPE Newsletter
IPE publishes a weekly eNewsletter, delivering a carefully chosen selection of the latest stories straight to your inbox.
Subscribe here