

Biscuit company returns to CSL
A leading biscuit manufacturer contacted Conveyor Systems Ltd (CSL) to provide a handling solution that involved transporting sealed cases of product up to high level on an inclined belt and merge with an existing CSL conveyor system that had been installed back in 2008 as part of a major £0.5m handling project.
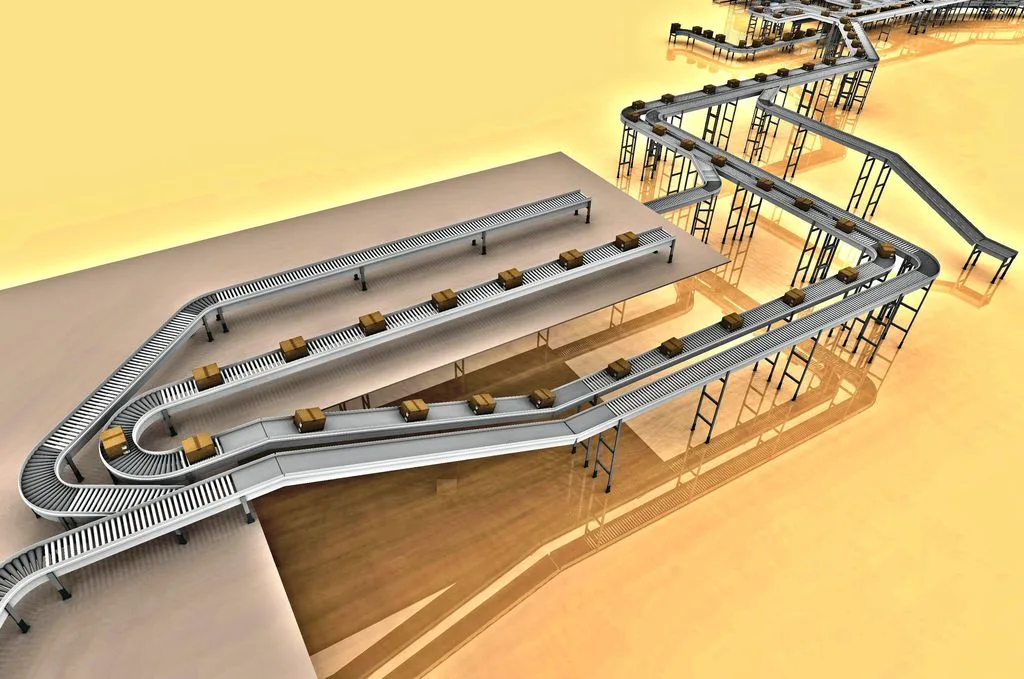
The system was designed to operate independently with its own control panel to keep downtime of the main system panel reduced to a minimum and allow maximum flow of other work in progress from an independent feed.
On exiting an automatic tape sealer, complete shelf ready pack (SRP) cases weighing 5kg run parallel with the existing main conveyor line, before they are transferred through a 180° powered roller bend due to restricted space, to be returned in the opposite direction before feeding up to a height of 2.5m via an inclined belt conveyor and on to a high level powered roller system.
The system incorporated 54m of powered roller conveyors, several bends and belt conveyors due to space restrictions, which necessitated over 12 changes in direction to enable it to thread its way through numerous obstacles within the roof space.
All the high level conveyors are suspended from roof trusses, bridging over existing conveyors and also maintaining clear floor access before the cases pass through a dividing wall and feed down a declining conveyor belt to merge with the existing large system.
With up to 35 cases per minute traversing the main line, a high speed merge was strategically positioned to space product out onto the line.
To avoid disruption to ongoing production, CSL worked out of hours and over week-ends in order to successfully complete the project to the customer’s satisfaction.
IPE Newsletter
IPE publishes a weekly eNewsletter, delivering a carefully chosen selection of the latest stories straight to your inbox.
Subscribe here