

Re-use of water: Savings pour in
When an old water purification plant at Parker Domnick
Hunter was no longer able to keep up with demand, Elga
Process Water came up with a cost effective solution that
also allows waste water to be re-used
Parker Domn
When an old water purification plant at Parker Domnick
Hunter was no longer able to keep up with demand, Elga
Process Water came up with a cost effective solution that
also allows waste water to be re-used
Parker Domnick Hunter manufactures
filtration, separation and purification
products for a wide range of
industries and applications. It uses a lot of
high purity water and water quality is critical
to maintaining high manufacturing quality
standard.
Derek Calder, manufacturing engineering,
explains: “Our filters go into many
pharmaceutical and food and beverage
systems, so water of pharmaceutical quality
is of paramount importance for flushing and
testing finished filters. Our production
schedule means that we need it 24/7.”
Increased production had pushed the
company’s pharmaceutical grade water usage
up to around 18,000L/h, and its old water
purification plant was no longer able to keep
up with the demand. It was time for a
replacement; but finding a plant of sufficient
capacity that could be installed in the available
space in the plant room without major loss
of production proved difficult. ELGA Process
Water, a division of Veolia Water Solutions &
Technologies came up with a solution.
In terms of water quality, ELGA Process
Water’s ORION packaged pharmaceutical
water system would have afforded a solution,
had it not been for the fact that the 6000L/h
output of the standard ORION was too small
to meet demand. ELGA Process Water’s
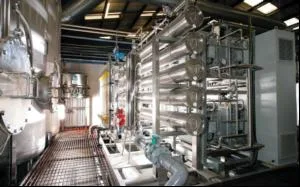
engineers set about designing a bespoke
system using similar process technology:
softeners followed by cartridge filters and then
a combination of reverse osmosis, continuous
electro-deionisation and ultrafiltration.
That was the easy part, as Dave Clarke,
project engineer, explains: “To minimise
production downtime we carried out most
of the work during phased out-of-hours
shutdowns.”
This included installing all the necessary
tanks, vessels and distribution loops which
would feed the production areas, while
production needs were still met by the old
plant. Installation of the new plant also
needed some thought. Clarke continues: “We
realised early on that the fully assembled
plant was too large to go through the plant
room doors, so we adopted a design based on
easily manoeuvrable, skid-mounted modules
that could be assembled inside the plant
room. The skids were designed to fit around
the constraints of the plant room floor.”
The specially designed plant was built and
assembled at ELGA Process Water’s factory in
Stoke-on-Trent and wet tested. After factory
acceptance testing and full validation the
plant was broken down into its component
skids and transported to site. Here, it was
rebuilt in it’s final position in the plant room
and re-commissioned. Parker Domnick
Hunter’s new plant was supplied with full
Design Qualification and Installation
Qualification documentation including the
URS, detailed design calculations, software
code review and drawings.Wet test and
calibration certificates met most of
Operational Qualification procedures and
final system validation on site was completed
swiftly. Eliminating the need for on-site
testing meant that the final changeover from
the old plant to the new one was achieved
quickly and without disrupting production.
ELGA Process Water was also responsible
for decommissioning the old plant, including
the safe disposal of chemicals, ion exchange
resins and similar waste materials – a task that
the company’s ion exchange resin regeneration
team carry out regularly and for which they
have all the necessary licences and procedures.
But even here a bit of thoughtful engineering
paid dividends: the reverse osmosis section
of the old plant was retained and connected
to recover the waste water from production.
It is now re-used as feed to the new plant,
reducing mains water consumption by about
50% and saving money.
ELGA Process Water’s water has a long
history of engineering bespoke
designs and a flexible
approach to ‘specials’. This,
together with the best
practices learned from half a
century of manufacturing
standard packaged plants
like the ORION, provided
Parker Domnick Hunter
with a cost effective
solution to its water
treatment challenge, with
minimum loss and with
the bonus of wastewater
recovery.
IPE Newsletter
IPE publishes a weekly eNewsletter, delivering a carefully chosen selection of the latest stories straight to your inbox.
Subscribe here