

Refreshing approach to parts supply
Coca-Cola European Partners’ (CCEP) plant is the largest soft drinks plant by volume in Europe.
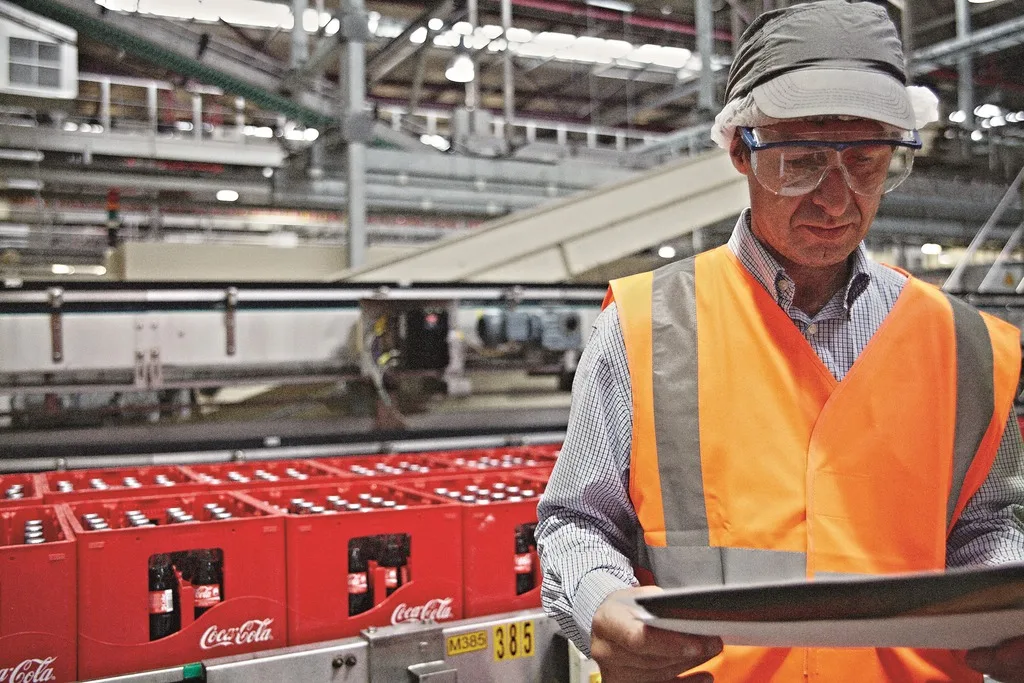
With a vast plant to maintain and a production schedule planned down to the second, CCEP partnered with Brammer, a leading Europe-wide distributor of industrial MRO products to manage the supply of its MRO spare parts to its manufacturing operations including its Wakefield site. Working with CCEP since 2009, the partnership has since evolved and is now based on a core concept of best practice in MRO procurement – vendor managed inventory. To achieve this, Brammer implemented its Insite service – effectively a dedicated branch housed within the Wakefield plant, achieving cost savings of more than 11% to date.
As well as savings generated through vendor consolidation and inventory rationalisation, the Insite team has been able to achieve significant savings through OEM conversion. Even worn or damaged components can be identified by the experienced team, and by sourcing replacement parts directly from the manufacturer rather than through the machinery OEM, Brammer has been able to cut costs as well as reduce lead times. In 2015, this project delivered a significant cost saving of 20% of usual annual spend.
Trevor Newman, Operations Director at CCEP Wakefield, explained: “The Insite™ team has undoubtedly been successful in reducing procurement costs and ensuring we at CCEP benefit from excellent inventory availability. But where Insite™ has added the greatest value for us is through the closely collaborative relationship we share, which enables the team to get out and about around the plant, proactively identifying potential projects to improve production efficiency and reduce costs.”
Insite manager Harry Strutt has been at the helm for four years, and explains: “We have quickly become a true extension of the in-house team meaning we’re always on hand to help with, and even identify, improvement projects. We recently worked on the Husky pre-form PET bottle presses which can create nearly a million pre-forms every 24 hours. We looked at the consumption of high-quality filtered hydraulic oil, and found that by installing an inline filtration system, we could reduce internal contamination and thus avoid damage to the critical components and valves within.
“As well as safeguarding the asset and improving component lifespan and reliability, the project has resulted in an overall saving of 26% per machine. And, inkeeping with CCEP’s CRS commitments, there’s been a reduction in the environment impact as fewer oil changes are needed therefore less oil needs to be disposed of.”
The Insite team also has extensive experience in the food and drink processing sector, enabling it to approach the challenges of a high-care manufacturing facility with ease. For example, bearings on various conveyor lines were failing prematurely due to frequent washdowns required coupled with heat from the drying process. By working closely with SKF as an authorised distributor of their bearings, Brammer was able to recommend the introduction of triple-sealed food grade bearings which have a service life of at least 18 months, compared to the three month typical life span of the previous bearings.
Trevor Newman concluded: “Many of the added-value projects managed by Brammer at Wakefield can also be replicated Europe-wide as every CCEP plant has its own Insite, meaning initiatives can result in cost savings many times over.”
IPE Newsletter
IPE publishes a weekly eNewsletter, delivering a carefully chosen selection of the latest stories straight to your inbox.
Subscribe here