

Ring machine
Designed for the high precision production of ringed turbine blade holders, the Excetek R2000 wire cut CNC EDM machine is available from UK and Eire agent, Warwick Machine Tools.
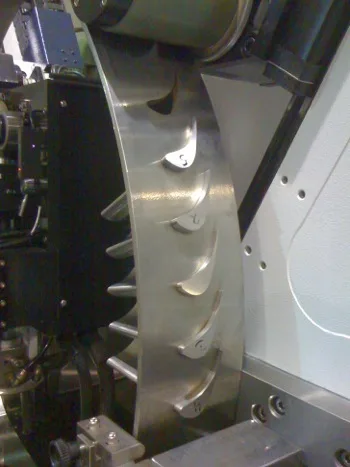
Able to accommodate rings with an outside diameter of between 600 and 2200mm with a wall thickness to 150mm, the R2000 can process workpieces to 300kg. Submerged wire cutting is carried out in the 800L work tank, with axis travels of 200 x 300 x 220mm in X, Y and Z respectively. U and V axis travels are 80mm, offering a maximum cutting taper angle of ±20°.
“The technical specification of the R2000 Ring Machine has been thoroughly evaluated by Excetek, to ensure the machine matches the demand from customers in the aero engine and thermal power generation sectors. It highlights the company’s willingness to invest in industry specific solutions,” states Ian Holbeche, MD of WMT.
With twin support spars intended to securely hold the ring material, the R2000 has a specially developed wire feed head designed to provide clear access to the inside diameter of the ring so that any blade location features or cooling feedways can be quickly and accurately machined.
All machine tool research and development is done in-house, and the software and high frequency pulse control generator have been created by Excetek. The CNC system has been developed by the company using Windows-based 64-bit architecture with a 15 inch LCD touch-screen for programming. Excetek says it is easier for operators to understand as they are already familiar with the ‘look and feel’ of the Windows environment. One day’s training is all that is required before the operator is competent to program and run the machine. Programming can be done using standard ISO G code or Excetek’s Icon Assistant conversational software, which uses the controls extensive database of cutting technologies.
While the cutting speed of every wire EDM machine is limited by the laws of physics and set by the thickness of the raw material being cut, it is a manufacturer’s corner control that defines its machine accuracy. Excetek’s software ensures the motion control and spark generator work together for the optimum power ramping and compensation dwell on corners, avoiding wire twist and reducing corner ‘washout’.
The structure of the R2000 wire EDM machine was designed using FEA software to provide exceptional accuracy in the linear axes movements and to minimise any thermal influence. The AC servo motor driven C1 class ball screws are cryogenically treated to minimise the thermal effects of the machine’s ambient operational environment, with high accuracy linear scales fitted for positional feedback.
Also developed by Excetek, the automatic wire feed and threading system is produced in-house. Designed to provide continuous unmanned operation around-the-clock, the AWT offers the ability to thread the wire at the point of the breakage. An automated annealing system straightens the wire so that it can be threaded at the break point during machining with almost 100% reliability and without the need to return to the start position. Submerged wire threading is possible, which removes the need to drain and refill the tank.
IPE Newsletter
IPE publishes a weekly eNewsletter, delivering a carefully chosen selection of the latest stories straight to your inbox.
Subscribe here