

Self-contained blast room upgrades production
Production facilities at
specialist pipeline valve
manufacturer, Oliver
Twinsafe, have been
upgraded with the installation
of a self-contained
Enviraclean blast room with
abrasive recovery system and
high-performance
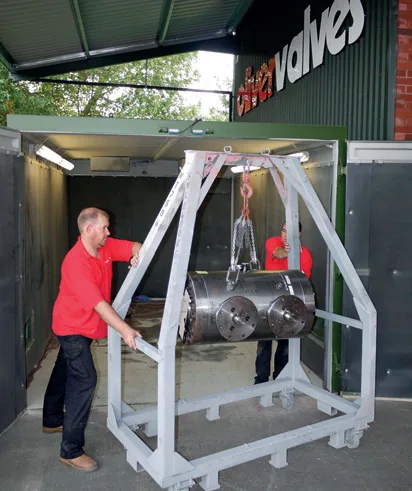
Production facilities at
specialist pipeline valve
manufacturer, Oliver
Twinsafe, have been
upgraded with the installation
of a self-contained
Enviraclean blast room with
abrasive recovery system and
high-performance sound
insulation from Hodge
Clemco.
The chamber measures 4m
long x 3m wide x 2.5m high
and has double access doors
at one end to accommodate
large components. The walls
are lined with rubber curtains
to reduce abrasion, and
modular double-skinned
panels have an acoustic lining
to reduce the noise that can
be heard outside the chamber
during blasting. Air inlet
ducts and exhaust outlets are
designed to provide effective
ventilation in order to ensure
good visibility for operators.
Media is projected by a
2452 SGV blasting machine
via a 3/8 inch (10mm) ID
tungsten-carbide-lined nozzle,
which is designed to maintain
maximum blasting velocity,
uniform abrasive distribution
and high work-rate over a
long operating life.
Abrasive is recovered for
re-use by means of a
pneumatic suction filter unit
linked to a sweep-in hopper
in the floor of the blast room.
IPE Newsletter
IPE publishes a weekly eNewsletter, delivering a carefully chosen selection of the latest stories straight to your inbox.
Subscribe here